Inspection Works Best When the Acceptance Standard Is Defined First.
At Botanicblossoms, inspection is connected to the approved product reference, written specification, color and appearance requirements, dimensions, assembly, finish, packaging, labels and order quantity.
Factory QC can support the order, and buyer-appointed or third-party inspection can be coordinated when required. The inspection method, sampling approach, acceptance criteria and release condition should be agreed for the actual project rather than assumed from a generic policy.
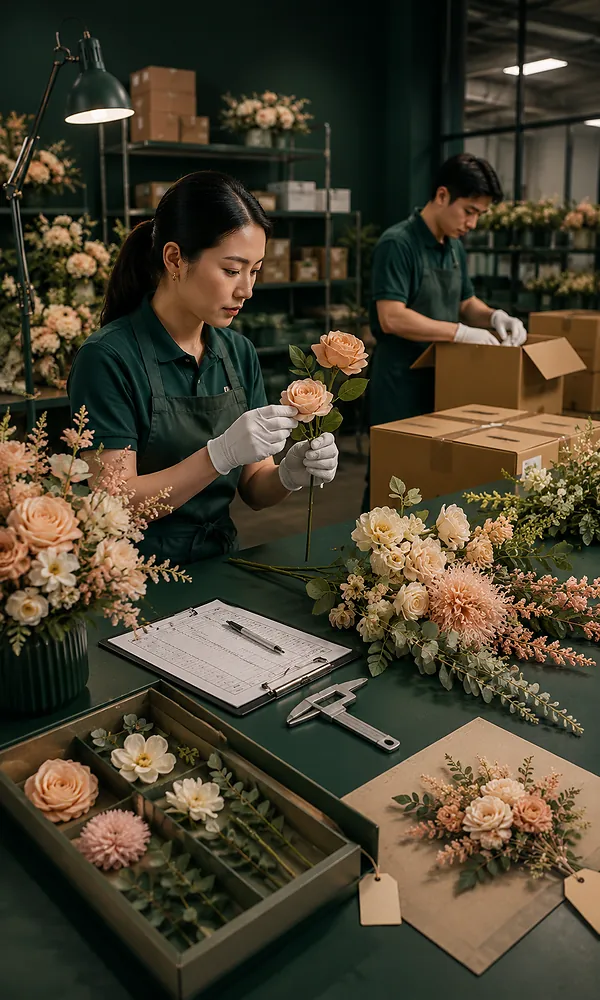

Sample · Specification · Pack · Label
“Looks Different” Is Not an Inspection Standard.
Buyers and factories need a controlled reference before inspection begins. Without it, color, shape, finish and packing can become subjective after production is already complete.
The Buyer Reviews One Sample, but Production Uses Another Version.
The approved sample, photo, drawing and written specification should identify the same production version.
Color or Shape Is Rejected Without an Agreed Comparison Method.
Lighting, material texture, bloom opening, canopy width and branch angle can affect visual judgment.
Product Inspection Passes, but Packing Is Checked Too Late.
Case pack, carton marks, protection method and product orientation can affect delivery quality.
Inspection Is Booked After the Shipping Cut-Off Becomes Critical.
The schedule should leave room for findings, corrective action and recheck before shipment release.
Inspection Needs a Controlled Reference Hierarchy.
The exact hierarchy should be agreed for the order. The goal is simple: the inspector should know which source controls when two references appear to conflict.
Physical or controlled visual reference where applicable.
Dimensions, materials, construction, finish and tolerance where agreed.
SKU, quantity, color, packaging and commercial identification.
Unit pack, case pack, carton mark and protective method.
Sampling, defects, tests or report format where specifically required.
If the buyer changes a critical requirement after approval, the new requirement should be incorporated into the controlled production and inspection reference before the order is judged against it.
Choose the Inspection Route to See What Needs to Be Defined.
Factory QC, buyer inspection and third-party inspection can all support quality control, but their scope and authority should be clear before the inspection date.
Internal Quality Control Supports Production and Final Release.
Factory QC can check the order against the approved production reference through manufacturing, final inspection and packing. Buyer-specific requirements should be provided before inspection begins.
Production consistency and order conformity.
Approved sample, written specification and any special inspection criteria.
Buyer-specific criteria introduced only after production is complete.
Buyer-Appointed Inspection Should Follow the Buyer’s Own Acceptance Standard.
The buyer or its sourcing agent can inspect the order when this is part of the agreed order process. The factory should receive the scope, timing and reference materials before the visit.
Buyer-defined product and packaging criteria.
Inspector contact, checklist, sampling approach and release authority.
Inspector arrives with criteria that were never communicated to production.
Independent Inspection Works Best with a Pre-Agreed Scope.
A buyer-appointed third party can inspect product, quantity, packaging or other defined items. The inspection company is not selected or endorsed by this general policy page.
Independent verification against buyer criteria.
Provider, booking, checklist, sampling plan and acceptance criteria.
The third party uses a default checklist that does not reflect the actual order.
Verify the Finished Order Before the Shipping Release Window.
Pre-shipment verification can focus on finished product conformity, quantity, packing, labels and shipment readiness according to the agreed scope.
Finished goods + packing readiness.
Final SKU list, packing standard, label requirements and release criteria.
Inspection occurs too close to the carrier cut-off for corrective action.
Verify the Shipment Identity at the Final Logistics Handover Stage.
Where required, a loading or dispatch check can confirm carton identity, quantities, visible packing condition and shipment allocation against the agreed logistics scope.
Cartons, shipment identity and dispatch allocation.
Packing list, shipment booking, carton marks and loading scope.
Loading check is mistaken for a complete product inspection.
Different Products Fail in Different Ways.
Select a product family to see the inspection points that normally deserve more attention.
Appearance, Bloom Shape and Stem Assembly Need a Visual Reference.
Artificial flowers combine color, petal construction, bloom opening, stem position and hand assembly. Inspection should compare the finished appearance against the agreed sample or specification.
Color, bloom opening, petal condition, stem construction and assembly.
Color reference, overall size and visual presentation.
Visual difference caused by shape or hand assembly rather than nominal dimensions alone.
Protect blooms and stems from excessive compression.
Leaf Density, Color, Branch Position and Pot Assembly Define the Final Look.
Artificial plants often combine repeated leaves, stems, internal supports and a base or planter. Inspection should review visual balance as well as assembly security.
Leaf density, branch position, color consistency, stem assembly and base stability.
Overall height, canopy width, leaf density and approved visual shape.
Correct height but visibly different density or branch distribution.
Protect foliage from excessive folding or permanent deformation.
Large Products Need Dimensional, Structural and Visual Inspection Together.
Artificial trees can include trunks, branches, detachable sections, foliage and planters. Height alone is not enough to describe the finished product.
Overall dimensions, canopy shape, connection security, trunk / branch finish and stability.
Height, canopy width, branch arrangement, assembly method and base requirement.
Loose connections, unstable assembly or shape variation after unpacking.
Secure sections and protect branches, foliage and surfaces during transport.
Dimensions, Surface Finish and Packing Protection Become Critical.
Planters and vases can have buyer-visible surfaces and fit requirements. Inspection should combine dimensional checks with finish and packaging review.
Dimensions, visible surface, color / finish, edge condition and base stability.
Critical dimensions, finish reference, acceptable visual variation and packing method.
Surface scratches, chips, inconsistent finish or incorrect dimensions.
Use separation, wrapping or localized protection according to the product.
Material-Specific Finish and Assembly Need Their Own Acceptance Criteria.
Decorative products can involve molded surfaces, coatings, welds, attachments, textures or hand-applied finishes. Inspection should follow the actual construction.
Surface finish, structure, attachments, coating, dimensions and visible defects.
Material / finish standard, dimensions, visual texture and functional assembly.
Treating intentional texture or handmade variation as the same thing as a production defect.
Protect hard surfaces, edges and attached components from impact and abrasion.
Inspection Should Cover the Product and the Order Around It.
The exact checklist depends on the SKU and buyer requirements, but these categories help prevent inspection from becoming only a visual spot check.
Correct SKU, Color, Size and Quantity.
Confirm that the inspected goods belong to the actual order and approved variant.
Compare Against the Approved Reference.
Review color, shape, visual balance, finish and buyer-defined appearance points.
Measure the Critical Dimensions That Matter to the Buyer.
Height alone may not describe canopy width, planter size or visual proportion.
Check Secure Assembly and Visible Finish Quality.
Leaves, stems, branches, bases, attachments and decorative surfaces should follow the approved standard.
Inspect What the Buyer Will Receive.
Unit pack, case pack, protective material, carton marks, labels and barcode requirements can be included where applicable.
Quality Release and Shipping Release Are Connected but Distinct.
Inspection status, packing completion and commercial release should all be resolved before dispatch.
Do Not Assume a Sampling Plan That the Buyer Never Approved.
If a buyer requires a specific sampling standard, defect classification, acceptance level, test method or inspection format, that requirement should be provided before the inspection is booked.
Botanicblossoms should not invent a universal AQL, sampling quantity or acceptance threshold for all product families. The order-specific inspection method should control.
Define How Units Are Selected.
Buyer or third-party requirements should state the sampling approach where applicable.
Define What Counts as a Defect.
Appearance, measurement, function or packaging issues should not be classified after the result is known.
Define Pass / Hold / Rework Logic.
Inspection results should connect to an agreed release decision.
Plan What Happens After Correction.
Recheck or reinspection should follow the buyer's agreed procedure when required.
A Finding Should Trigger a Controlled Response — Not an Argument.
Select an issue type to see a practical corrective logic.
Compare the Finding Against the Approved Color / Appearance Reference.
Confirm which batch, SKU and comparison reference are involved before deciding whether the deviation is real and order-relevant.
Isolate the Affected Goods and Correct the Confirmed Deviation.
Correction can involve sorting, reshaping, replacement, rework or another project-specific action depending on the actual issue.
Recheck the Corrected Goods Against the Same Controlled Reference.
The release decision should follow the agreed inspection or buyer procedure after correction.
Measure the Critical Dimension and Confirm the Agreed Visual Geometry.
Separate true dimensional nonconformity from visual shape differences such as canopy width, branch angle or bloom opening.
Correct the Dimension, Assembly Position or Shape Where Technically Possible.
The corrective route depends on whether the issue comes from cutting, assembly, shaping, component selection or another production step.
Re-Measure and Re-Compare the Finished Shape.
Use the same dimension definition, measurement method and approved visual reference during recheck.
Identify the Loose, Misaligned or Visually Unacceptable Assembly / Finish Point.
Compare the affected component, connection, surface or finish against the approved product construction.
Rework or Replace the Confirmed Assembly / Finish Issue.
Correction can include securing components, adjusting assembly, cleaning, refinishing or replacing affected parts depending on the product.
Verify Security, Appearance and Function After Rework.
Recheck the corrected goods against the same assembly and finish requirements before release.
Compare Packing, Labels and Carton Identity Against the Approved Order.
Confirm case pack, unit pack, protective materials, barcode, label, carton mark and shipment allocation where applicable.
Repack, Relabel or Correct Carton Allocation Before Shipment.
The affected cartons should be isolated so the correction does not create a new SKU or quantity error.
Recount and Reverify the Corrected Shipment Data.
Confirm the final packing and label status before logistics release.
The Inspector Should Know the Scope Before Arriving at the Factory.
Botanicblossoms can coordinate factory access for buyer-appointed or third-party inspection where required by the order. The buyer should confirm the provider, inspection scope, timing, acceptance criteria and release authority in advance.
This page does not claim a partnership with any inspection company. The buyer may nominate its preferred inspection provider subject to project coordination.
Buyer Confirms the Inspector.
Share inspector contact details and booking information early.
Define What the Inspector Must Check.
Product, packaging, labels, quantity, sampling and buyer-specific tests where applicable.
Book at the Correct Completion Stage.
Inspection should be scheduled when the order is sufficiently ready for the requested scope.
Define Who Authorizes Release.
Pass, hold, correction or reinspection logic should follow the buyer's order procedure.
Inspection Complete Does Not Automatically Mean Shipment Released.
Quality status, packaging, corrective action, commercial terms and shipping arrangements may all need to be complete before dispatch.
Complete the Agreed Inspection.
Use the controlled sample, specification and buyer criteria.
Resolve Findings Where Required.
Sorting, rework or another corrective action depends on the actual issue.
Confirm the Corrected Status.
Recheck or reinspection follows the agreed order procedure.
Confirm Quality + Packing + Commercial Release.
Shipment proceeds only after the applicable order conditions are complete.
Requirement → Reference → Readiness → Inspection → Findings → Correction → Recheck → Release
Select a stage to see what should be complete before the inspection process moves forward.
Define What the Inspector Is Expected to Verify.
The process begins with the buyer’s required product, packaging, quantity, labels, sampling method and release criteria where applicable.
SKU list, approved standard, inspection scope and buyer-specific criteria.
Acceptance criteria are still being negotiated when inspection starts.
Inspector and order team understand what must be checked and how the result will be used.
Lock the Approved Sample, Specification and Order Version.
The inspector should use a controlled reference that matches the current order and production version.
Approved sample / photos, specification, color reference, PO and packing standard.
The factory, buyer and inspector are using different versions.
One controlled inspection reference is identified.
Inspect at the Right Production and Packing Stage.
The order should be sufficiently complete for the intended inspection scope, while leaving time for corrective action if needed.
Production completion status, packing status, inspector booking and shipment schedule.
Inspection occurs before enough goods are ready or too close to shipping cut-off.
The order is ready for the planned inspection scope.
Execute the Agreed Checks Against the Controlled Standard.
Inspect product identity, appearance, dimensions, assembly, finish, quantity, packaging and other buyer-defined criteria as applicable.
Inspector, checklist, samples / units, measurement tools and reference materials.
Unapproved new criteria are introduced during inspection.
Findings are recorded against the agreed scope.
Classify Findings Against the Agreed Criteria.
A finding should identify the SKU, issue, evidence and applicable reference before a corrective decision is made.
Inspection evidence, affected quantity / sample information and reference comparison.
Subjective comments are treated as confirmed defects without reference.
Confirmed deviations are separated from acceptable variation or non-applicable comments.
Correct the Confirmed Nonconformity at the Appropriate Production Level.
Correction may involve sorting, rework, reshaping, repacking, relabeling or another product-specific action.
Confirmed issue, affected goods and approved corrective route.
Correction fixes one problem but creates SKU, appearance or packing inconsistency elsewhere.
Affected goods are corrected and ready for recheck.
Verify the Corrected Goods Against the Same Reference.
Recheck or reinspection should follow the buyer’s agreed procedure and use the same acceptance logic.
Corrected goods, original finding, reference and recheck scope.
The recheck uses a different or less strict standard than the original inspection.
Quality status is resolved under the agreed procedure.
Connect Quality Release to Packing, Commercial and Shipping Release.
A completed inspection should feed into the final order-release process together with packing completion and applicable commercial conditions.
Inspection status, recheck result where needed, final packing status and order release conditions.
Goods are dispatched while corrective or release conditions are still open.
The order is cleared for the next agreed shipping step.
Inspection Is Connected to a Real Production and Quality-Control Process.
Botanicblossoms operates an approximately 3,500 m² production facility in Jinhua, Zhejiang, with 51–100 employees, including 5–10 R&D personnel, and monthly production capacity of around 500,000 units.
Quality control is integrated from material selection and manufacturing through inspection, packaging and shipment. OEM/ODM projects can also introduce custom colors, materials, sizes, finishes, molds and private-label packaging that should be reflected in the inspection reference.
Send Inspection Requirements →Reliable Inspection Starts by Avoiding Claims the Order Cannot Support.
This page explains how inspection can be structured. It does not invent a universal inspection standard that applies to every artificial flower, tree, planter or decorative product.
Sampling Must Follow the Actual Buyer Requirement.
Do not assume one acceptance level across all products and projects.
Quality Results Depend on the Actual Order.
Do not publish an unsupported inspection pass percentage.
Buyer May Nominate Its Own Provider.
This page does not fabricate partnerships with third-party inspection companies.
Use Defined Criteria and Corrective Control.
Trust is stronger when inspection and correction logic are explicit.
Questions Buyers Should Resolve Before Inspection Is Booked.
The buyer's approved reference and order-specific inspection criteria should control the actual inspection.
What do you inspect before shipment?
The inspection scope depends on the product and order. Common categories can include SKU identity, color and appearance, dimensions, assembly, finish, quantity, packaging and labels. Buyer-specific tests or criteria should be provided before inspection.
Do you use a fixed AQL for every order?
This policy does not publish a universal AQL or sampling level. If your company requires a specific sampling standard, acceptance level or defect classification, provide it before the inspection is scheduled.
Can I appoint my own inspection company?
Buyer-appointed or third-party inspection can be coordinated where required by the order. Share the provider, inspection scope, timing and contact details early so factory access can be arranged.
When should third-party inspection be booked?
The booking point depends on the inspection scope. It should be scheduled when the relevant quantity and packing status are sufficiently complete for the inspector to perform the required checks, while still leaving time for corrective action if needed.
What happens if inspection finds a problem?
The finding should be compared against the approved order standard. If a confirmed deviation requires correction, the affected goods can be isolated and corrected according to the actual issue, followed by recheck or reinspection where required.
Can inspection include packaging and labels?
Yes, where included in the inspection scope. Unit packing, case pack, protective packaging, carton marks, private-label artwork, barcode or other buyer-defined packaging requirements can be reviewed against the approved standard.
Is a passed inspection the same as a product certification?
No. An order inspection verifies the agreed inspection scope for that shipment. Product testing, certification or compliance documentation is a separate subject and should be supported by the actual applicable evidence.
Does inspection guarantee zero defects?
Inspection is a quality-control process, not a blanket zero-defect guarantee. Its reliability depends on the approved standard, inspection scope, sampling method where applicable, execution and corrective-action process.
What information should I send before inspection?
Send the SKU list, quantity, approved sample or specification, critical dimensions, color reference, packaging and label requirements, sampling method, defect criteria, report format and release procedure where applicable.
Inspection Routes, Acceptance Logic and Corrective Control.
It explains how approved references, factory QC, buyer inspection, third-party inspection, packing checks, findings and release can be structured.
Universal AQL, Fixed Sampling, Guaranteed Pass Rate or Zero Defects.
The actual inspection should follow the order-specific reference, buyer criteria and agreed inspection procedure.
Send the Acceptance Standard Before the Inspector Arrives.
Share the product, SKU quantity, approved sample or specification, color reference, critical dimensions, packaging, labels, sampling method, third-party inspector information and required release criteria.